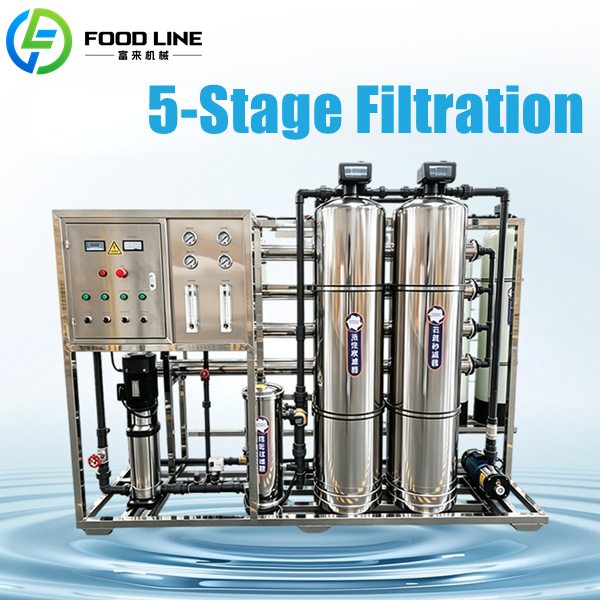
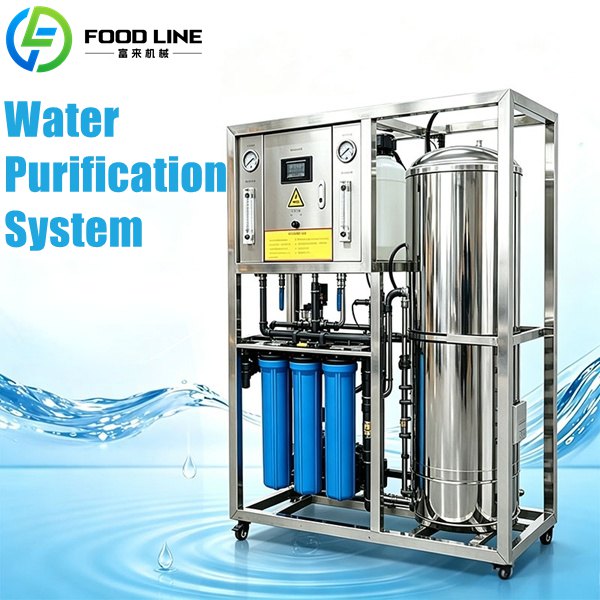
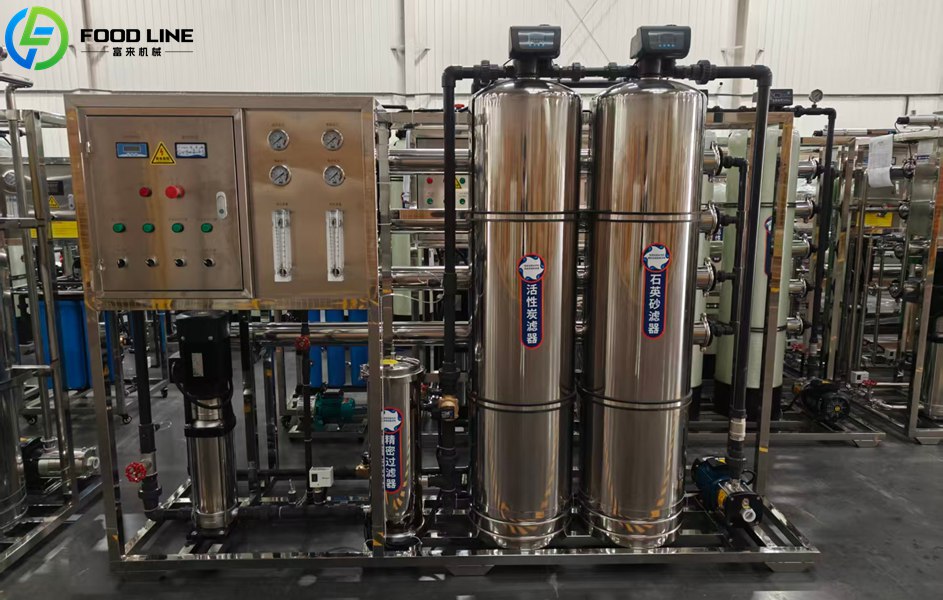
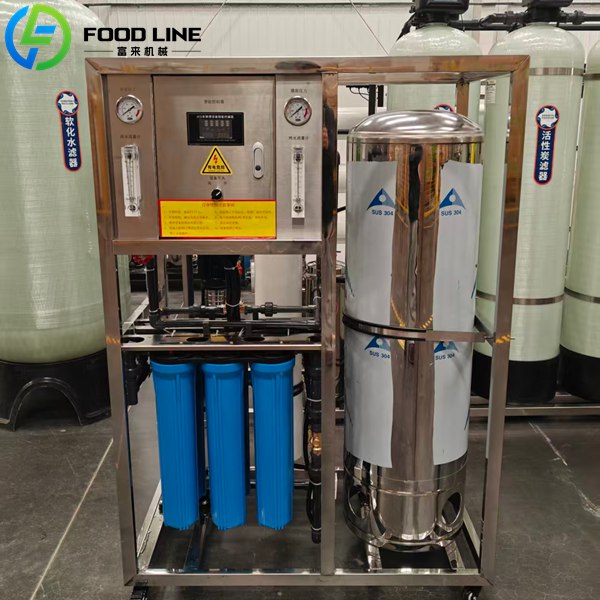
In industrial production, water quality affects product quality, equipment operating efficiency, and production costs. Industrial water purifying machine are used in the electronics manufacturing, food processing, and pharmaceutical industries. Our equipment incorporates pretreatment, softening, precision filtration, and reverse osmosis processes. It can reduce suspended solids, silt, residual chlorine, and dissolved impurities in raw water. Request factory prices! WhatsApp/Phone: +86 13838385752
Water Purifying Machine Parameters
Applicable Raw Water
Municipal tap water, well water, groundwater, etc.
Operating Temperature
Optimal range: 8 – 25°C
Shutdown Conditions
Recommended to stop operation when water temperature > 35°C or < 8°C
Equipment Inlet (Raw Water) Pressure
0.02 – 0.4 MPa
Pre‑pump Pressure
0.02 – 0.1 MPa
Post‑pump Pressure
0.5 – 1.5 MPa
Concentrate (Brine) Pressure
0.5 – 1.5 MPa
Power Supply
220V or 380V, configured according to single‑phase / three‑phase and on‑site grounding conditions
Precision Filtration Rating
5 μm PP sediment filter cartridge
Contact Us! WhatsApp/Tel: +86 138 3838 5752
commercial purified water equipment
Industrial Water Purifying Machine Overview
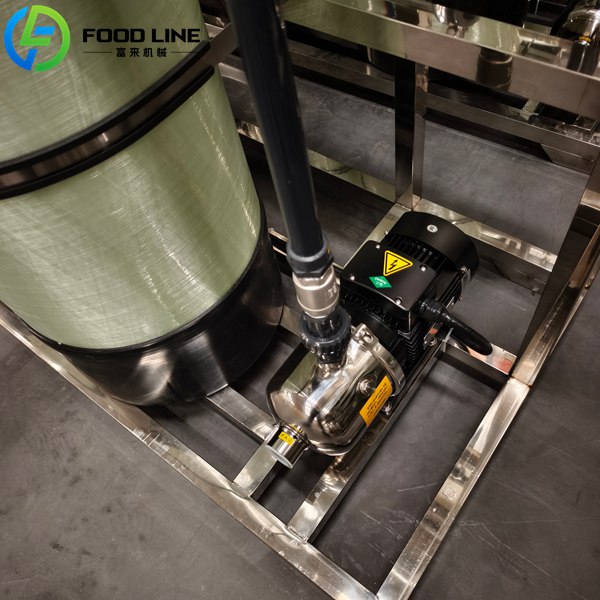
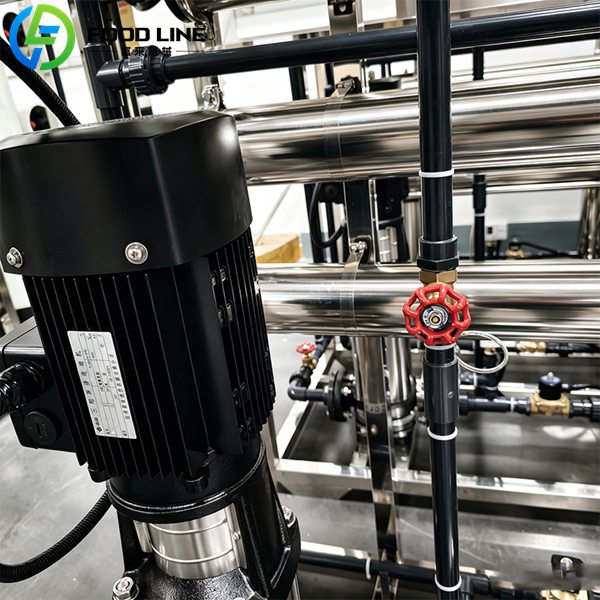
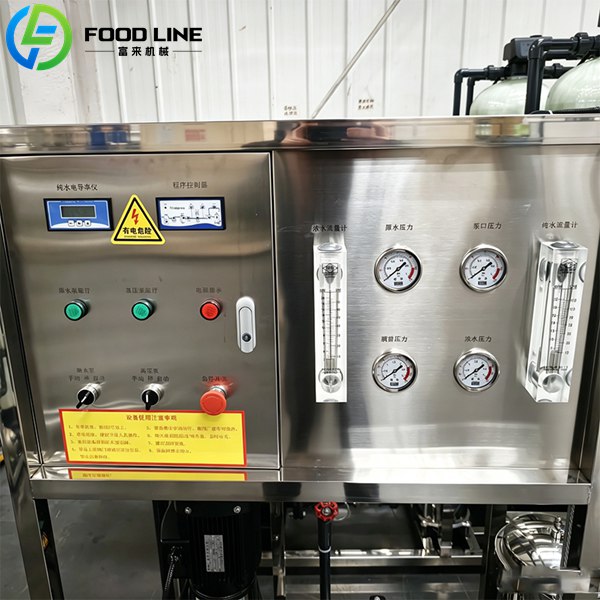
It mainly consists of a raw water tank, a pure water tank, a raw water pump, a high-pressure pump, a quartz sand filter, an activated carbon filter, a softening resin tank, a scale inhibitor dosing device, a precision filter, an RO reverse osmosis membrane module, a flow meter, a pressure gauge, an inlet solenoid valve, an automatic multi-way valve, an RO controller, and a conductivity meter.
Process Flow
Raw Water Tank → Raw Water Pump → Quartz Sand Filter → Activated Carbon Filter → Scale Inhibitor Dosing → Precision Filter → RO Reverse Osmosis Unit → Pure Water Tank
Working Principle
This system employs reverse osmosis water treatment technology. After passing through a filter, a high-pressure pump sends the pretreated water into the RO membrane housing. Under pressure, water molecules permeate through the reverse osmosis membrane to form permeate. Salt, hardness ions, and other impurities are discharged on the concentrate side. The permeate then enters a pure water tank for use in the production line.
Multi-stage pretreatment: This system consists of a pretreatment system comprising quartz sand, activated carbon, softening resin, scale inhibitor, and a precision filter. Pretreatment reduces RO membrane fouling and scaling.
Automatic multi-way valve control: The equipment can be configured with an automatic multi-way valve to achieve backwashing, forward washing, regeneration, and switching between operating programs.
Operating pressure and flow rate: The equipment monitors raw water pressure, pump inlet pressure, pump outlet pressure, concentrate pressure, permeate flow rate, and concentrate flow rate. Operators can promptly assess the equipment status using pressure gauges and flow meters.
Level and low-pressure protection: When the raw water tank is low on water, level protection prevents the pump from running dry. When the pure water tank reaches a high level, the system can stop water production or enter standby mode.
Manual debugging and automatic operation: After the equipment is installed, manually confirm that each component is operating normally before switching to automatic operation mode.
Stability: The equipment can progressively reduce the contamination load based on different raw water conditions, preventing untreated raw water from entering the reverse osmosis membrane.
Cost: Regular cleaning of the components can extend the lifespan of the filter media. Replace the 5μm PP filter cartridge when the differential pressure of the precision filter reaches 0.05 MPa to prevent clogging and a decrease in feed water flow.
Discharge: The system’s concentrate, backwash water, and flushing water can be supplied with independent or combined discharge pipelines. Concentrate valve adjustment can ensure water quality while optimizing recovery rate.
About Foodline
Before purchasing equipment, Foodline will develop a matching pretreatment and reverse osmosis solution based on the customer’s factory, voltage, and water source to avoid equipment incompatibility with site conditions. If you are building a water plant, we also offer backend equipment: block ice machines, tube ice machines, and flake ice machines for connecting to water purification equipment. Please contact us for a customized quote! WhatsApp/Phone: +86 13838385752